TIG Welding (GTAW)
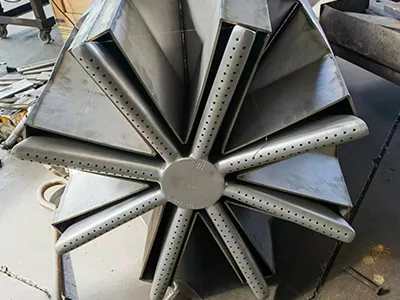
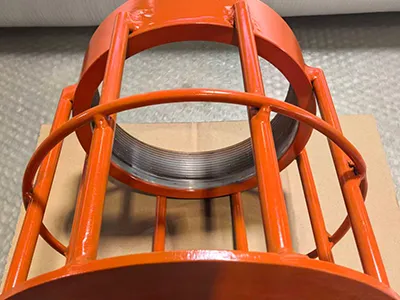
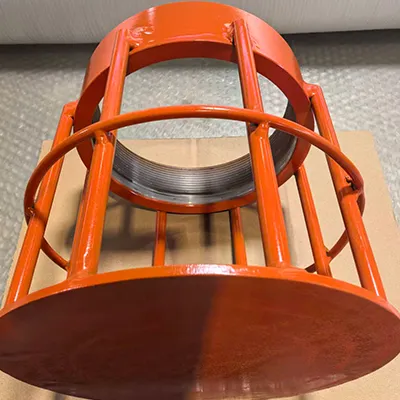
TIG welding (GTAW) uses argon as a shielding gas to protect the weld area and a non-consumable tungsten electrode to generate the welding arc. The process is well suited for thin-wall components and offers high weld quality, minimal distortion, and precise weld control.
We commonly use this for piping, precision components, and general-purpose vessels, primarily in carbon steel and stainless steel materials.
Our current welding capabilities support sheet metal thicknesses from 0.5 to 10 mm and pipe sizes from DN15 to DN600, with a minimum pipe wall thickness of 1.5 mm.
 Water Pump Filter
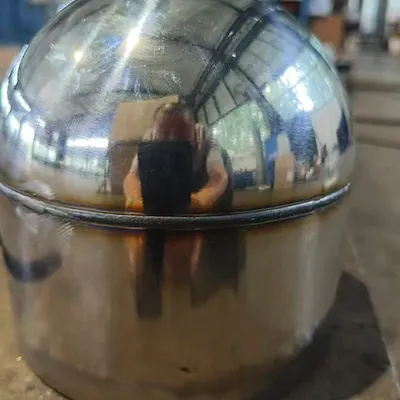 Water Valve Float Ball
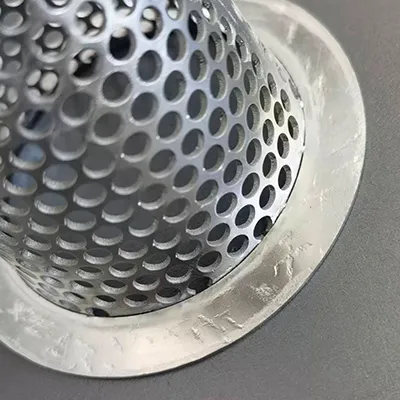 Filter
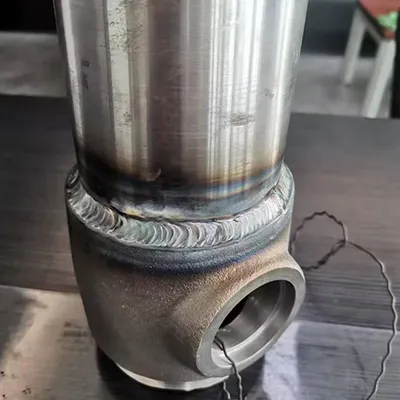 Tee Fitting
Material
- Stainless Steel
AISI/ASTM: 304, 304L, 316, 316L
EN: 1.4301 (304), 1.4307 (304L), 1.4401 (316), 1.4404 (316L)
JIS: SUS304, SUS304L, SUS316, SUS316L - Carbon Steel
ASTM: A36
EN: S235JR (1.0038)
Characteristics
- Exceptional Weld Quality and Cleanliness
Argon shielding protects the weld pool from atmospheric contamination, producing dense, porosity-free welds with no slag and minimal post-weld cleaning. - Excellent Weld Appearance
Precise control of heat input creates smooth, uniform welds with an excellent surface finish. Ideal for components with high aesthetic and surface-quality requirements. - All-Position Welding Capability
Excellent weld pool control enables flat, vertical, and overhead welding. The process is particularly well suited for thin-wall materials, minimizing the risk of burn-through.
Why Choose Huacheng
- More than 30 years of manufacturing and export experience, with extensive knowledge of international logistics and industry-specific technical standards.
- Full support from tooling design and sample development through to high-volume production, precision machining, and surface treatment.
- A strict ISO 9001 quality management system, backed by CMM (coordinate measuring machine) inspection and non-destructive testing (MT, RT, PT).